Food Processing
Tanks, piping and equipment requiring clean, corrosion-resistant welds to hygiene standards.
The premier choice for welding 304L, 304 and similar austenitic stainless steels. Low carbon content minimises carbide precipitation, ensuring maximum corrosion resistance in the as-welded condition — with smooth arc, easy slag removal and all-position versatility.
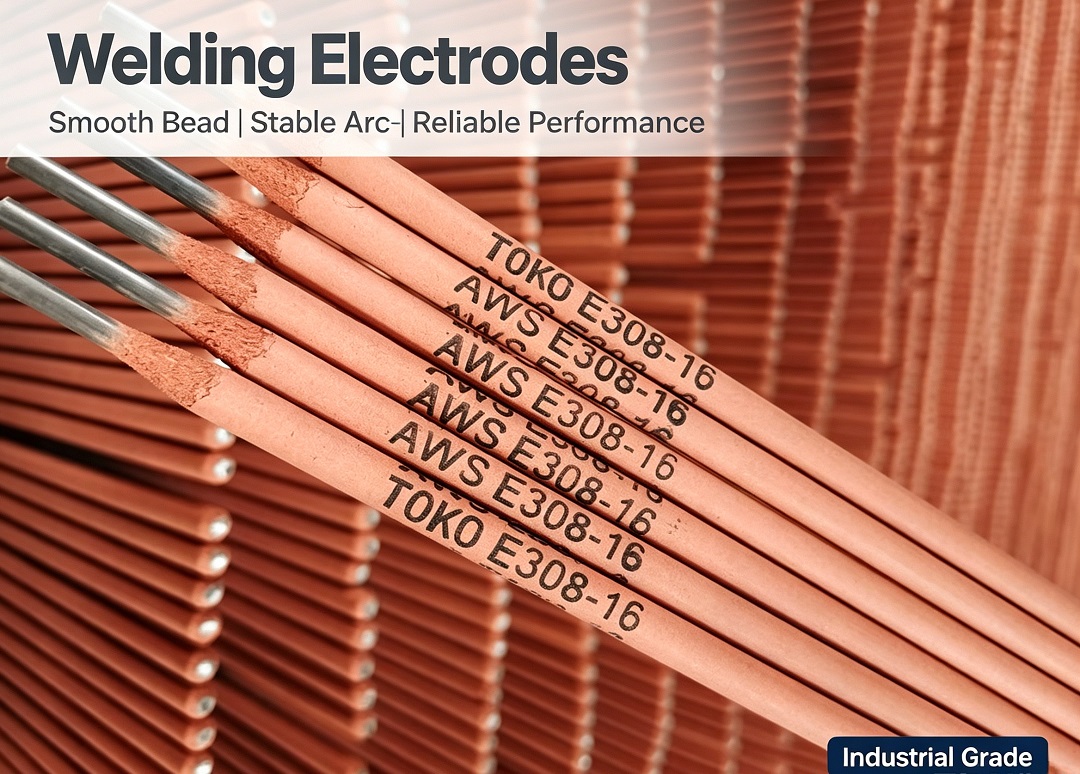
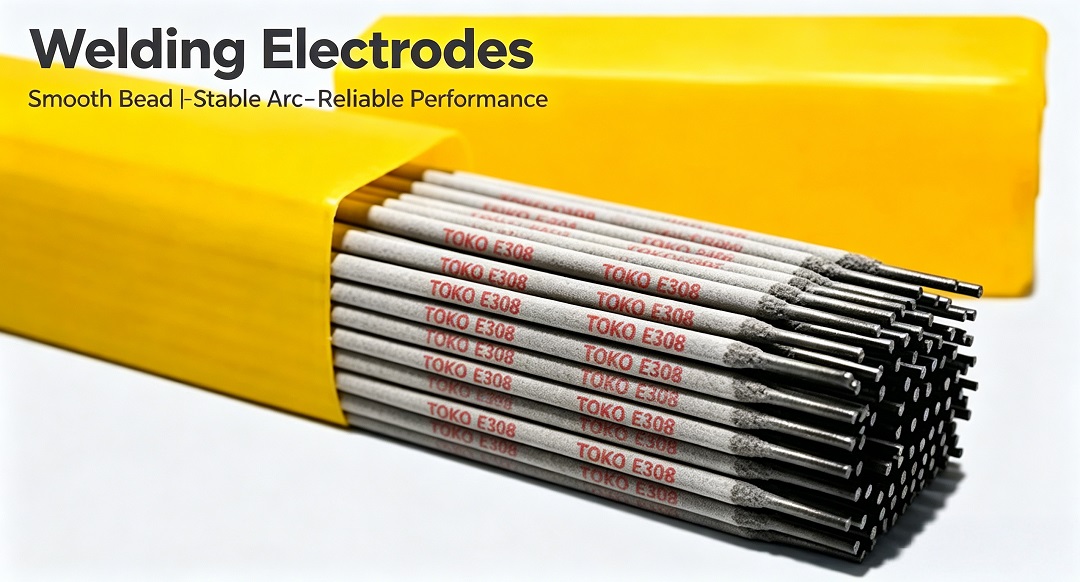

TOKO E308L-16 is a rutile-coated, low-carbon stainless steel stick electrode designed for welding austenitic stainless steels such as 304L, 304 and 321. The controlled carbon content (≤ 0.04%) provides excellent resistance to intergranular corrosion in the as-welded condition, while the rutile coating delivers a smooth, stable arc and self-detaching slag.
Not sure which stainless steel electrode fits your application? The table below summarises the differences between the three most common austenitic stainless steel electrode grades.
| Feature | E308L-16 | E316L-16 | E309L-16 |
|---|---|---|---|
| Base Metal | 304 / 304L stainless | 316 / 316L stainless | Dissimilar joints |
| Chemistry | 18–21% Cr, 9–11% Ni | 17–20% Cr, 11–14% Ni, 2–3% Mo | 22–25% Cr, 12–14% Ni |
| Key Property | Low carbon, general corrosion resistance | Molybdenum-enhanced pitting resistance | Dilution tolerance, dissimilar welding |
| Typical Applications | Food equipment, chemical tanks, 304L piping | Marine, pharmaceutical, chemical processing | Stainless to carbon steel, cladding |
| Max Service Temp. | ~400 °C continuous | ~400 °C continuous | ~300 °C continuous |
Full chemical composition, mechanical properties, welding parameters and storage guidelines for TOKO E308L-16 stainless steel electrode.
| Element | Value (%) |
|---|---|
| Carbon (C) | ≤ 0.04 |
| Chromium (Cr) | 18.0 – 21.0 |
| Nickel (Ni) | 9.0 – 11.0 |
| Manganese (Mn) | 0.5 – 2.5 |
| Silicon (Si) | ≤ 1.0 |
| Phosphorus (P) | ≤ 0.040 |
| Sulfur (S) | ≤ 0.030 |
| Copper (Cu) | ≤ 0.75 |
| Molybdenum (Mo) | ≤ 0.75 |
| Property | Value |
|---|---|
| Tensile Strength (MPa) | ≥ 550 (typical 580–620) |
| Yield Strength (MPa) | ≥ 350 |
| Elongation (%) | ≥ 35 |
| Hardness (HB) | ~ 180 |
| Ferrite Content (FN) | 3 – 10 (typical 5) |
| Diameter (mm) | Current (A) | Voltage (V) |
|---|---|---|
| 2.5 | 60 – 90 | 21 – 24 |
| 3.2 | 80 – 120 | 22 – 26 |
| 4.0 | 110 – 160 | 24 – 28 |
DCEP (DC+) recommended for optimal arc stability. Use short arc and preheat only if required by base metal thickness. Maintain interpass temperature ≤ 150 °C to avoid hot cracking.
| Condition | Requirement |
|---|---|
| Unopened packaging | Store in dry place (< 60% RH) |
| Opened electrodes | Use within 8 hours, or hold at 100–150 °C |
| Re-drying (if damp) | 250–300 °C for 1 hour |
Store in original hermetically sealed packaging. Moisture ingress can cause porosity and reduce corrosion resistance.
Trusted in industries where hygiene, durability and corrosion resistance are paramount.
Tanks, piping and equipment requiring clean, corrosion-resistant welds to hygiene standards.
Reactors, storage vessels and piping for mild chemical environments.
Handrails, facades and structural stainless steel components exposed to weathering.
Dairy equipment, pharmaceutical machinery and brewery installations.
Interior fittings, railings, and non-critical marine structures.
Service down to −196 °C where austenitic stainless toughness is essential.
E308L has a controlled maximum carbon content of 0.04%, which reduces the risk of chromium carbide precipitation during welding. This makes E308L the preferred choice for applications requiring maximum corrosion resistance in the as-welded condition, especially when welding 304L base metal.
The suffix -16 indicates a rutile-based coating with a potassium silicate binder. It is designed for use with AC or DCEP (DC+) and provides a smooth arc, easy slag removal and excellent all-position weldability. It is the most common and versatile variant for stainless steel electrodes.
Yes, E308L is perfectly suitable for welding 304 stainless steel. Its low carbon content provides extra assurance against sensitization, especially if the welded component will be exposed to corrosive environments. For 304L base metal, E308L is the standard choice.
Preheat is generally not required for austenitic stainless steels like 304L when using E308L. However, for thick sections (over 20 mm) or highly restrained joints, a maximum interpass temperature of 150 °C is recommended to avoid hot cracking. Post-weld heat treatment is typically not necessary.
Standard MOQ is one pallet (approximately 1–2 tons). Typical production lead time is 15–25 days for stock grades and 25–35 days for custom packaging or private-label orders. Free samples are available for qualified buyers.
Tell us your base material, welding position, standard and monthly volume. Our welding engineers will recommend the right diameter and confirm chemistry compliance, and send a full quotation with mill certificates and shipping options.
Download batch-specific material certificates, safety data sheets and welding procedure guidelines. All certifications are third-party verified and comply with AWS A5.4 / ASME SFA-5.4.