Chemical Processing
Reactors, vessels and piping for acids, chlorides and aggressive chemical environments.
The molybdenum-bearing 17Cr/12Ni electrode engineered for welding 316 and 316L stainless steels. Excellent resistance to pitting and crevice corrosion in chloride and acid environments — the standard choice for marine, chemical and pharmaceutical installations.

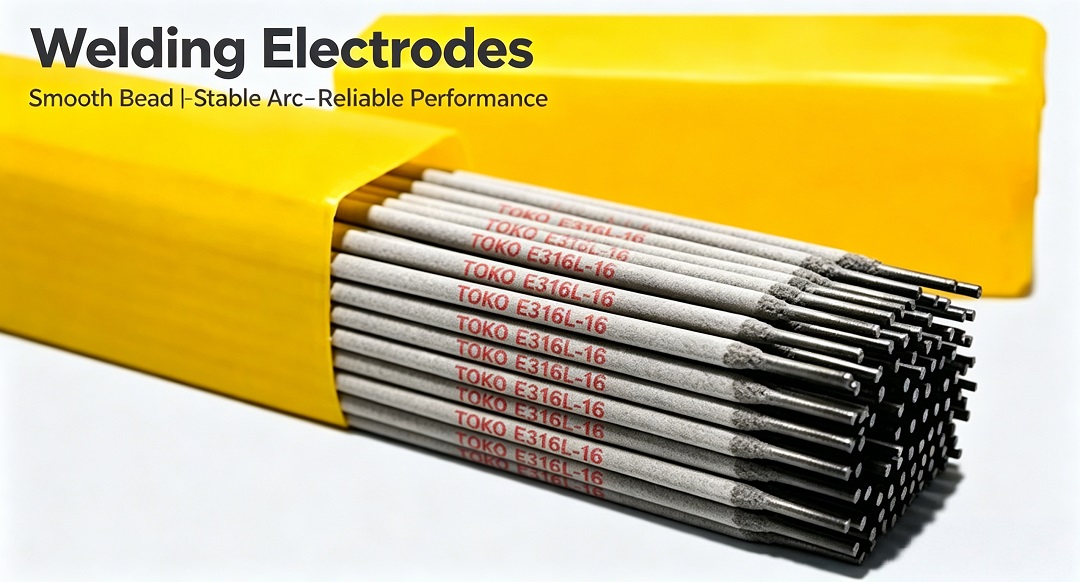

TOKO E316L-16 is a lime-titania coated, extra-low-carbon stainless steel stick electrode with a molybdenum-bearing 17Cr/12Ni chemistry. The 2–3% molybdenum addition dramatically improves resistance to pitting and crevice corrosion — particularly in chloride and acid environments. This makes E316L-16 the standard electrode for 316 and 316L base metals, marine structures, chemical processing equipment and pharmaceutical installations where maximum corrosion resistance is essential.
Not sure which stainless steel electrode fits your application? The table below summarises the differences between the three most common austenitic stainless steel electrode grades.
| Feature | E316L-16 | E308L-16 | E309L-16 |
|---|---|---|---|
| Base Metal | 316 / 316L stainless | 304 / 304L stainless | Dissimilar joints |
| Chemistry | 17–20% Cr, 11–14% Ni, 2–3% Mo | 18–21% Cr, 9–11% Ni | 23–25% Cr, 12–14% Ni |
| Key Property | Mo-enhanced pitting & crevice resistance | Low carbon, general corrosion resistance | Dilution tolerance, dissimilar welding |
| Typical Applications | Marine, chemical, pharmaceutical, 316L piping | Food equipment, chemical tanks, 304L piping | Stainless to carbon steel, cladding |
| Max Service Temp. | ~400 °C continuous | ~400 °C continuous | ~300 °C continuous |
Full chemical composition, mechanical properties, welding parameters and storage guidelines for TOKO E316L-16 molybdenum-bearing electrode.
| Element | Value (%) |
|---|---|
| Carbon (C) | ≤ 0.04 |
| Chromium (Cr) | 17.0 – 20.0 |
| Nickel (Ni) | 11.0 – 14.0 |
| Molybdenum (Mo) | 2.0 – 3.0 |
| Manganese (Mn) | 0.5 – 2.5 |
| Silicon (Si) | ≤ 1.0 |
| Phosphorus (P) | ≤ 0.040 |
| Sulfur (S) | ≤ 0.030 |
| Copper (Cu) | ≤ 0.75 |
| Property | Value |
|---|---|
| Tensile Strength (MPa) | ≥ 520 (typical 550–600) |
| Yield Strength (MPa) | ≥ 350 |
| Elongation (%) | ≥ 30 |
| Hardness (HB) | ~ 180 |
| Ferrite Content (FN) | 3 – 10 (typical 5) |
| PREN (Pitting Resistance Equivalent) | ≥ 24 |
PREN = %Cr + 3.3 × %Mo + 16 × %N. A PREN ≥ 24 indicates enhanced resistance to pitting corrosion in chloride environments.
| Diameter (mm) | Current (A) | Voltage (V) |
|---|---|---|
| 2.5 | 60 – 90 | 21 – 24 |
| 3.2 | 80 – 120 | 22 – 26 |
| 4.0 | 110 – 160 | 24 – 28 |
DCEP (DC+) recommended for smoothest arc. AC also suitable. Use short arc and maintain interpass temperature ≤ 150 °C for thick sections.
| Condition | Requirement |
|---|---|
| Unopened packaging | Store in dry place (< 60% RH) |
| Opened electrodes | Use within 8 hours, or hold at 100–150 °C |
| Re-drying (if damp) | 250–300 °C for 1 hour |
Store in original hermetically sealed packaging. Moisture ingress can cause porosity and reduce corrosion resistance.
Trusted in industries where superior corrosion resistance in chloride and acid environments is essential.
Reactors, vessels and piping for acids, chlorides and aggressive chemical environments.
Hull structures, seawater piping, desalination plants and offshore platforms.
Sterile processing equipment, fermentation vessels and sanitary piping.
Digesters, bleach plants and chemical recovery equipment.
Shell-and-tube exchangers, condensers and cooling water systems.
Scrubbers, flue-gas desulphurisation (FGD) systems and wastewater treatment.
E316L-16 contains 2–3% molybdenum in addition to 17–20% chromium and 11–14% nickel, whereas E308L-16 contains no deliberate molybdenum. The molybdenum addition significantly improves resistance to pitting and crevice corrosion in chloride and acid environments — making E316L-16 the preferred electrode for 316/316L base metals, marine structures, chemical processing equipment and pharmaceutical installations.
Yes, E316L-16 is the correct matching electrode for 316 and 316L stainless steels. Its extra-low carbon content (≤0.04%) minimizes carbide precipitation, and the molybdenum addition provides pitting resistance equivalent to the base metal.
Molybdenum increases the pitting resistance equivalent number (PREN) of the weld metal. Even small additions (2–3%) greatly enhance resistance to pitting and crevice corrosion in chloride-containing environments such as seawater, brine, and many organic and inorganic acids.
E316L-16 is suitable for service temperatures up to approximately 400 °C, though long exposure to the 450–850 °C range should be avoided because of sigma-phase formation. For higher temperatures or more aggressive conditions, higher-alloyed grades or nickel-based electrodes are preferred.
Standard MOQ is one pallet (approximately 1–2 tons). Typical production lead time is 15–25 days for stock grades and 25–35 days for custom packaging or private-label orders. Free samples are available for qualified buyers.
Tell us your base material, welding position, standard and monthly volume. Our welding engineers will confirm chemistry and PREN suitability, and send a full quotation with mill certificates and shipping options.
Download batch-specific material certificates, safety data sheets and welding procedure guidelines. All certifications are third-party verified and comply with AWS A5.4 / ASME SFA-5.4.